CNC Hydraulic Relief Pressing
数控液压浮雕机多道次压制
标签:数控压机, 多道次, 力-位移曲线, 聚氨酯垫
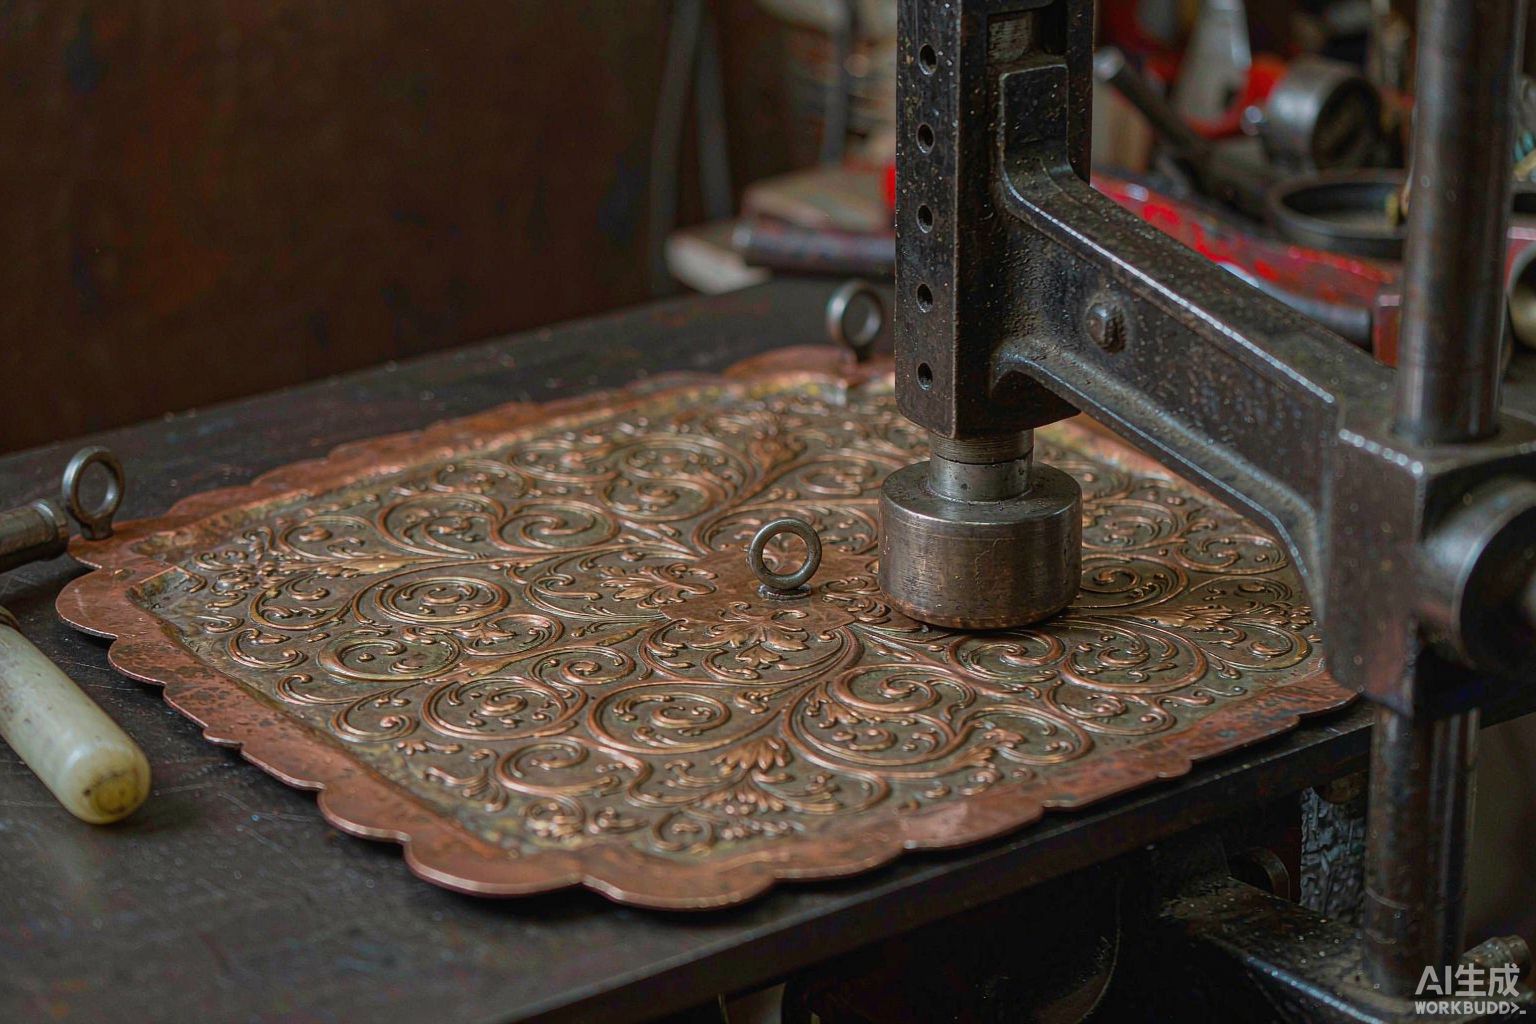
数控液压浮雕机压制 1.5 mm T2 铜板浮雕(深厚比 2.5:1)的标准路线:压力 120–300 t,滑块速度分两段——接近板面时降至 5 mm/s、压制段 8–15 mm/s,末段保压 3–5 s 让材料流动充分。板下垫 30 mm 邵氏 A90 聚氨酯垫均布压力,分 3 道次渐次压深,道次间 550 °C 退火。力-位移曲线编程可锁定峰值吨位防止尖角压穿,同一程序批间一致性 ±2%,是手工浮雕无法达到的复现性。
For pressing 1.5 mm T2 copper relief at 2.5:1 depth-to-gauge on a CNC hydraulic press: 120–300 t force, two-stage ram speed—slow to 5 mm/s on approach, 8–15 mm/s during forming, then dwell 3–5 s for full flow. A 30 mm Shore-A 90 polyurethane pad equalises pressure. Press in three passes with 550 °C anneals between. Programming the force-displacement curve caps peak tonnage at thin features; batch repeatability is ±2%, far beyond hand work.